
- WEBSITE -

Current location: HOME > NEWS > Frequently Asked Questions >
Analysis of Key Precautions for the Assembly and Welding of Color Steel Roll Forming Machines
Time:2026-10-29 05:06:27 Author:xiangyi Click:60
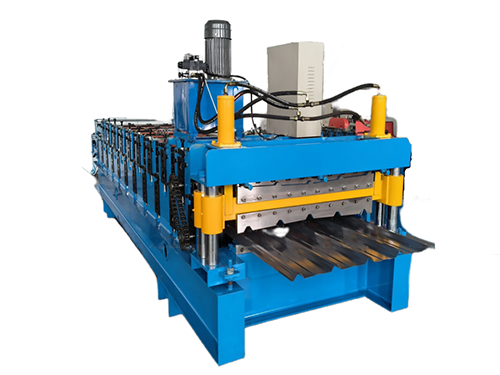
The assembly and welding quality of a color steel roll forming machine directly determines its overall rigidity,forming precision,and long-term operational stability.As the core load-bearing structure of the equipment,improper control of the welding process can easily lead to deformation,stress concentration,weld cracking,and roller axis deviation.These issues can further affect the straightness of the formed panels,cutting precision,and the equipment's service life.Therefore,during the assembly and welding process,systematic control must be implemented across material preparation,welding processes,assembly precision,deformation control,post-weld treatment,and quality inspection.
Material and Process Preparation Before Welding
Before assembly and welding,the steel grade,thickness,and specifications used for the frame should be confirmed according to the equipment drawings to ensure that material dimensions meet design requirements.Roll forming machine frames are typically welded from structural steel,steel plates,or square tubes.Since different parts serve different functions,the welding materials must match the base metal.For carbon steel frames,electrodes or welding wires with strength comparable to the base metal should be prioritized.If CO2 gas shielded welding is used,it is essential to ensure that the welding wire specifications,gas flow rate,and welding parameters meet the process requirements.
Welding materials must be stored properly to prevent moisture,rust,or contamination.Low-hydrogen electrodes should be baked according to specifications before use to prevent porosity,slag inclusions,or hydrogen-induced cracking in the welds.The welding area must be kept clean;oil,rust,scale,and moisture on both sides of the groove and weld must be removed to ensure good fusion.
Assembly Precision Determines Overall Forming Quality
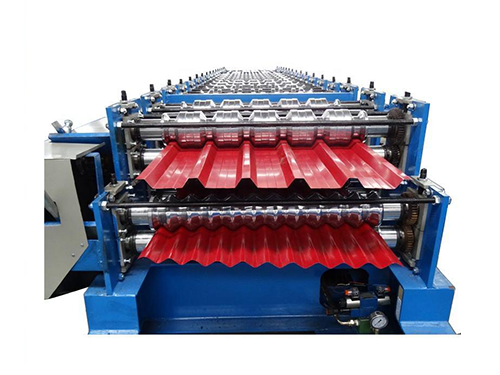
As a continuous cold roll forming equipment,the dimensional precision between the frame,side plates,bearing seats,and roller mounting positions is critical.During assembly,positioning,leveling,and alignment should be carried out according to the drawings to ensure that the left and right side plates are parallel,the bearing holes are coaxial,and the guide rail mounting surfaces are flat.Tack welds should not be too long or too high and should be evenly distributed to avoid excessive local stress.For long frames or large frameworks,multi-point positioning should be used,and diagonals,flatness,and key mounting hole positions should be checked to prevent overall twisting after subsequent welding.
Assembly gaps should be controlled within a reasonable range.Excessive gaps increase the amount of filler metal,leading to greater deformation and residual stress;insufficient gaps may cause incomplete penetration or poor fusion.For mating surfaces that require subsequent machining,welds should be avoided in precision machining areas to prevent affecting machining precision and surface quality.
Proper Selection of Welding Methods and Parameters
In the assembly and welding of roll forming machines,CO2 gas shielded welding,manual metal arc welding(MMAW),and argon arc welding(TIG)are common.CO2 gas shielded welding offers high production efficiency and stable weld formation,making it suitable for main frame welding;MMAW is highly flexible and ideal for local repair welding and confined spaces;TIG welding is suitable for areas with high requirements for weld appearance and formation quality.
Welding parameters should be reasonably adjusted according to plate thickness,joint type,and welding position.Excessive current can easily cause burn-through,undercut,and an enlarged heat-affected zone;insufficient current can lead to incomplete penetration,slag inclusions,and poor weld formation.For thin plates,a lower heat input and controlled welding speed should be used to avoid excessive local heating and warping.During multi-pass welding,each pass should be cleaned thoroughly,and interpass temperature should be kept moderate to prevent structural coarsening and stress concentration.
Strict Control of Welding Sequence to Reduce Frame Deformation
Welding sequence is a critical factor in controlling frame deformation.Generally,the principle of"short welds before long welds,internal welds before external welds,and symmetrical welds before asymmetrical welds"should be followed.For frame structures,symmetrical welding,back-step welding,or welding from the center towards both ends can be adopted to distribute heat more evenly and reduce overall shrinkage deformation.
When multiple welders work simultaneously,weld points should be scattered to avoid heat concentration in the same area.Long welds should not be welded continuously at once;segmented welding or skip welding can be used to reduce local heat accumulation.For thin-walled structures with low rigidity,temporary supports or anti-deformation measures can be set up before welding if necessary,so that the dimensions after weld shrinkage are closer to the design requirements.
Post-Weld Stress Relief and Precision Calibration
After welding,significant residual stress will exist inside the frame.If used directly,the equipment may experience dimensional drift,weld cracking,or reduced forming precision during long-term operation.Therefore,important frames should undergo stress relief treatment after welding,such as vibratory stress relief or thermal treatment,to stabilize structural dimensions and improve overall rigidity.
After stress relief,key mounting surfaces,bearing seat holes,and guide rail datum surfaces of the frame should be re-measured.If flatness,parallelism,or hole position deviations exceed the allowable range,timely calibration or machining should be performed to ensure that the roller axes are parallel and the clearances are uniform after installation.Only with a stable frame datum can the roll forming machine ensure smooth material feeding,regular profiles,and accurate cut-to-length.
Weld Appearance Inspection and Anti-Corrosion Treatment
After welding,an appearance inspection of the welds should be conducted.Qualified welds should have uniform formation and smooth transitions,with no cracks,porosity,slag inclusions,incomplete penetration,severe undercutting,or obvious weld spatter.For load-bearing parts,key connection points,and long welds,special attention should be paid to whether the fusion condition and weld height meet the drawing requirements.
Weld surface cleaning is equally important.After welding,slag,spatter,and oil should be removed promptly,and the welds and surrounding areas should be ground.Since roll forming machine frames are mostly made of carbon steel,the heat-affected zone is prone to rust.Therefore,after cleaning,anti-rust primer should be applied promptly or overall anti-corrosion coating should be carried out to prevent rust during transportation,storage,and use.
Safety and On-Site Management During Assembly
Assembly and welding operations must strictly comply with safety operating procedures.Welders must have the corresponding qualifications,and equipment such as welding machines,cables,grounding,and protective devices should be checked before operation.The welding site should be well-ventilated,free of flammable materials,and equipped with fire extinguishers.During high-altitude operations or when flipping and hoisting large frames,dedicated lifting points should be set up,and overloading or rough handling is strictly prohibited.
During assembly,all temporary supports,positioning blocks,and fixtures should be removed only after welding is completed and dimensional stability is confirmed.Before the equipment is transferred to the next process,the main dimensions of the frame,weld quality,anti-rust status,and assembly records should be verified to ensure that every roll forming machine has a stable structural foundation before leaving the factory.Through standardized assembly and welding management,not only can the overall precision of the equipment be improved,but the professionalism and reliability of the manufacturing process can also be demonstrated to overseas customers.
CONTACTS
Contact:+86 15075795678
URL:www.xiangyirollformingmachine.com
ADD:Jiajializhuang Village, Bo Town, Botou City, Cangzhou City, Hebei Province, China